Explore our flagship soccer uniforms engineered for pro-tier performance clubs, collegiate academies, retail private labels, and high-velocity tournament distributors worldwide.
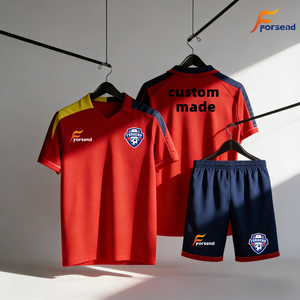
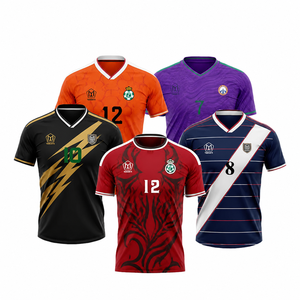
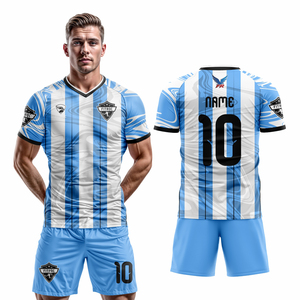
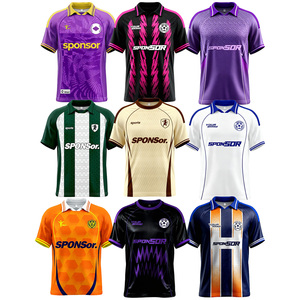
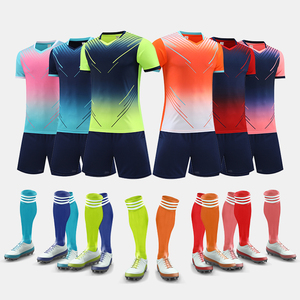
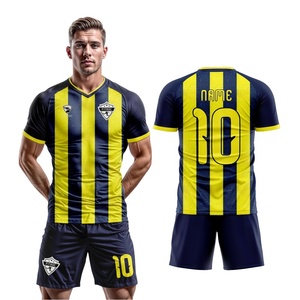
Operating directly within the globally renowned sporting goods manufacturing cluster of Defence Road, Sialkot, Pakistan, our vertically integrated plant eliminates intermediaries to guarantee tight quality controls, audited CE compliance, and reliable CIF/FOB export timelines.
We maintain strict control over 75D/72F micro-denier polyester yarn sourcing, circular knitting machines, and proprietary hydrophilic finishes. This ensures optimal capillary moisture dispersion, robust burst strength, and zero static buildup under extreme pitch friction.
Every garment exported complies with CE marking safety protocols, European REACH Annex XVII (zero banned aromatic amines, zero nickel release on zips, and zero formaldehydes), and OEKO-TEX Standard 100 Class I safe-skin criteria for both youth and adult league play.
Equipped with multi-head Swiss laser cutters and Japanese industrial dye-sublimation print engines, our factory achieves 0.2mm pattern registration, flawless Pantone solid coated color fidelity, and edge-to-edge sublimation that never fades, cracks, or peals under commercial 60°C laundering.
Supportive of both boutique athletic brands and high-volume importers. Starting from flexible minimums of 50 units per design, we engineer bespoke jacquard collars, heat-welded silicone crests, high-density embroidered badges, custom woven neck tags, and barcoded retail polybags.
Our international documentation office drafts exact Commercial Invoices, GSP Form A (Generalized System of Preferences) certificates of origin where applicable, detailed packing lists, and bill of lading (B/L) filings to ensure frictionless customs clearance at UK, European, US, and Australian ports.
Turnaround tech pack briefs into tangible pre-production master samples within 5 to 7 working days. Every pre-production jersey undergoes strict inspection for GSM density, seam elongation (ASTM D1683), and wash-durability before your team greenlights bulk cutting.
Professional B2B soccer jersey procurement requires granular clarity on yarn parameters, burst resistance, and functional knitting profiles. Below is our factory's standard production grade comparative breakdown:
| Performance Tier | Primary Yarn & Weave | Weight (GSM) | Air Permeability | Bursting Force | Colorfastness (ISO 105) | CE / REACH Status |
|---|---|---|---|---|---|---|
| Pro Match Player Version | 75D/72F Recycled Micro-Polyester Jacquard w/ Elastane Mesh | 135 - 145 GSM | > 180 cm³/cm²/s | > 420 kPa (ASTM D3786) | Grade 4.5 - 5.0 | Pass / Fully Certified |
| Club Commercial Fan Replica | 100% Filament Polyester Flat Interlock Weave | 150 - 165 GSM | > 140 cm³/cm²/s | > 480 kPa (ASTM D3786) | Grade 4.0 - 4.5 | Pass / Fully Certified |
| Academy Training & Youth Set | 100% High-Tenacity Bird-Eye Poly Mesh | 140 - 150 GSM | > 210 cm³/cm²/s | > 510 kPa (ASTM D3786) | Grade 4.0 - 4.5 | Pass / Fully Certified |
| Vintage Heritage / Retro Series | Heavyweight Cotton-Touch Interlock Poly Weave | 180 - 200 GSM | > 95 cm³/cm²/s | > 560 kPa (ASTM D3786) | Grade 4.5 | Pass / Fully Certified |
As professional clubs, retail brands, and athletic academies prepare for the 2026/2027 fiscal cycles, commercial procurement teams must anticipate shifts in sustainable sourcing directives, agile manufacturing protocols, and advanced surface functionalization.
Regulatory mandates across the European Union and North America are transitioning performance sportswear from virgin polyester to post-consumer recycled polyethylene terephthalate (rPET). Modern rPET filaments now match virgin polymers in tensile strength, dye-affinity, and wickability while reducing carbon output by up to 34% per jersey produced. Procurement directors must secure verified GRS transaction certificates (TC) to substantiate their retail eco-claims.
Heavy chemical silver-ion finishes are rapidly being superseded by bio-derived antimicrobial agents derived from peppermint oil and renewable chitosan polymers. Simultaneously, micro-encapsulated phase change materials (PCM) printed onto targeted heat-generation zones (spine, lower lumbar, underarms) are entering the pro-tier market, proactively buffering skin temperature through latent heat absorption and release during 90-minute high-intensity match conditions.
While digital all-over sublimation remains the undisputed champion for complex match kit graphics, high-tier commercial branding demands textured contrast. The market is shifting decisively toward combining high-definition disperse-dye sublimation with ultrasonic thermo-bonded 3D silicone badges, matte metallic crests, and laser-cut heat transfer numbers. This hybrid technique preserves featherweight jersey ergonomics while delivering prestigious retail sensory appeal.
To mitigate inventory holding costs and deadstock risks, global kit distributors are adopting dual-track procurement: pre-booking foundational greige fabric lots with our factory months in advance, then releasing rapid digital print and cut-and-sew orders in smaller, staggered drops (100–300 pcs) linked dynamically to tournament qualifications, league promotions, or mid-season sponsor alterations.
Overseas apparel procurement involves navigating complex trade-offs between unit cost, tariff classification, lead-time variance, and factory compliance audits. Implementing an institutionalized sourcing framework guarantees operational resilience.
Metamerism and shade shifting between production batches are major causes of retail returns. Professional buyers must mandate that their manufacturer knit and dye greige polyester in uniform master lots. Our Sialkot facility utilizes automated spectrophotometer lab dip color measurement (ΔE < 0.8 tolerance under D65 daylight, TL84 store light, and incandescent light sources) to guarantee 100% shade replication across repeat re-orders.
Navigating ocean vs. air cargo economics is pivotal for seasonal tournament rollouts. By coordinating directly from our factory via Port Qasim/Karachi for sea containers (22–28 days to European/North American hubs) or direct air-freight out of Sialkot International Airport (SKT) for critical replenishment (4–6 days), importers achieve optimal cash flow balancing while keeping landed duty-paid costs competitive.
We enforce the internationally accepted ISO 2859-1 (ANSI/ASQC Z1.4) Sampling Plan at AQL 2.5 Major / 4.0 Minor for all export consignments. Inline quality control technicians examine seam tension (4-thread overlock with double-needle topstitch), bar-tack reinforcement at tension stress zones, zipper smoothness, and dimensional stability following five successive industrial laundering cycles.
Critical guidance for sourcing managers, apparel brand founders, and teamwear directors seeking clarity on CE certified soccer uniform manufacturing in Sialkot, Pakistan.
In European and international sports apparel sourcing, CE certification verifies that the soccer jerseys conform to strict European Union health, environmental, and consumer safety directives—specifically General Product Safety Directive (GPSD 2001/95/EC), flammability standards under EN 14878 (where applicable to youth garments), and chemical safety thresholds regulated by REACH Regulation (EC) No 1907/2006 Annex XVII. This ensures the textiles contain zero banned azo dyes, toxic heavy metals (lead, cadmium), carcinogenic dispersants, or phthalates. Our factory provides third-party test reports validating that our soccer apparel is completely compliant and ready for unimpeded commercial import across all EU and global member states.
For full custom cut-and-sew soccer jerseys (tailored yarn selection, proprietary Pantone dye matching, bespoke collar jacquards, and customized pattern sizing), our standard manufacturing MOQ begins at just 50 pieces per design/colorway, which can be distributed across standard sizing splits (e.g., Youth XS–XL through Adult S–3XL). For repeat orders or blank sublimation-ready stock garments, MOQs can be further optimized based on your procurement volume. Larger production runs exceeding 500 units unlock enhanced bulk yarn pricing and reduced sea-freight freight consolidation rates.
Dye migration (sublimation gas bleeding into adjacent polyester panels or vinyl numbers) is eliminated through a multi-step chemical fixation process. We utilize high-purity disperse sublimation inks possessing high molecular weight, formulated to bond permanently within the amorphous regions of the polyester fiber at 205°C to 215°C under uniform calibrated pneumatic roller pressure. Finished fabrics achieve a tested Colorfastness to Washing rating of Grade 4.5 to 5.0 (ISO 105-C06), Colorfastness to Perspiration of Grade 4.5 (ISO 105-E04), and Colorfastness to Rubbing of Grade 4.5 (ISO 105-X12).
Our standard production lifecycle follows an organized 4-phase milestone schedule:
1. Digital Proofing & Lab Dip Approval: 2–3 business days.
2. Physical Pre-Production Sample Fabrication: 5–7 business days (couriered via DHL/FedEx with tracking).
3. Mass Bulk Production & Assembly: 15–20 business days for orders ranging from 200 to 2,500 pieces upon physical sample sign-off.
4. Inline QC, Packaging & FOB Handover: 2 business days.
For time-sensitive tournament requirements, accelerated rush production runs can be scheduled with dedicated sewing lines.
Yes. While we maintain standardized international sizing profiles (US Athletic, European Pro Fit, and Asian Standard Slim Cut), our automated CAD pattern drafting software accepts proprietary size charts submitted in Excel, PDF, or DXF tech pack formats. We accurately grade across chest width, sleeve length, bicep circumference, front/back hem drop, and neck opening curves. In addition, we manufacture tailored women's ergonomic football silhouettes, unisex youth sizing, and adult plus sizes up to 5XL.
Our Defence Road facility integrates comprehensive embellishment capabilities under one industrial roof:
• Full Continuous Dye-Sublimation: Zero-hand feel on all-over polyester graphics.
• High-Definition Ultrasonic 3D TPU Badges: Dimensional textured club crests with metallic, holographic, or matte finishes.
• High-Density Multi-Head Embroidery: Up to 12 colors with satin fill and tatami underlay.
• Silicone Heat Transfer Printing: High-stretch player numbers and corporate sponsor wordmarks that resist cracking under elastane fabric elongation.
• Woven Merrowed Crests & Damask Labels: Flawless micro-text definition for neck labels and lower hem authenticity jock tags.
We operate under transparent, globally standard banking terms designed to safeguard commercial buyers. Standard initial orders are typically transacted via T/T (Telegraphic Transfer) with an advance production deposit (typically 30% to 50%) upon pre-production physical sample approval, and the final balance settled upon presentation of inspection photos/videos and standard B/L shipping documents. For established enterprise partners, verified distributors, and recurring institutional contracts, we readily accept Irrevocable Letters of Credit (L/C at sight) and structured staggered supply terms.
Speak directly with our technical pattern engineers and export sales team in Sialkot, Pakistan. Receive itemized FOB/CIF quotation matrices, sample scheduling, and certified fabric swatch books tailored precisely to your brand's specifications.
