
Pro Match Grade
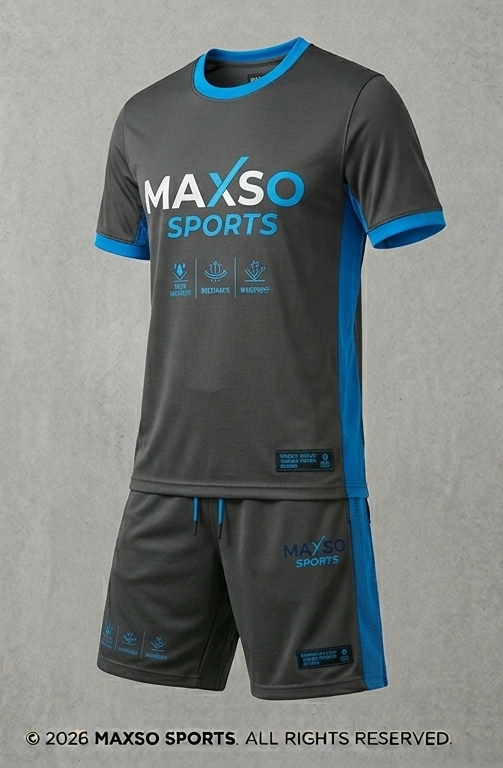
Pro-Elite Sublimated Soccer Kit
Style Code: MS-SUB-SOC-01- Fabric
- 150 GSM Interlock + Jacquard Mesh
- Printing
- Full Body Sublimation (Italy Inks)
- Stitching
- Reinforced Flatlock / Double Needle
- MOQ
- 50 Sets (Custom Sizes S-3XL)
Sourcing high-performance sublimation soccer uniforms requires an in-depth understanding of fabric technology, dye-sublimation chemistry, and precision cut-and-sew manufacturing. Maxso Sports, operating directly out of Sialkot, Pakistan, manufactures professional-grade, zero-fade, custom-printed football kits for sports brands, professional clubs, regional leagues, and teamwear distributors across the US, UK, Canada, Australia, and Europe.


Why do elite football clubs and international federations choose custom sublimated soccer uniforms over conventional screen printing or heat transfers? The secret lies in polymer chemistry and thermochemical molecular bonding.
Unlike traditional screen printing, which lays a heavy, rubbery layer of plastisol ink on top of the fabric, or vinyl heat transfers that block micro-vents, dye sublimation printing converts solid ink pigments directly into a gas state under high temperature (195°C – 205°C) and pressure (4 to 5 bar). This gas penetrates open synthetic micro-polyester polymer fibers. As the material cools, the fibers close, permanently trapping the dye inside the yarn itself rather than sitting on top.
This chemical process creates a completely weightless garment. The fabric retains 100% of its native breathability, softness, tensile stretch, and moisture-wicking capillary action. Crucially for high-intensity soccer matches, sublimated soccer uniforms will never peel, crack, flake, or fade—even after hundreds of industrial laundry cycles at high temperatures.
Ultra-lightweight, smooth micro-denier weave engineered for maximum speed, rapid sweat evaporation, and frictionless skin contact during 90+ minutes of competitive play.
Body-mapped mesh side panels designed with 3D structural air pockets that increase airflow velocity across core body heat zones by up to 38%.
Formulated with eco-certified non-toxic dyes providing a wide color gamut (Oeko-Tex Standard 100 compliant) for vibrant Neon, Pantone solid, and deep gradient matching.
Explore our battle-tested uniform specifications developed for pro clubs, youth academies, semi-pro leagues, and private label activewear brands.
Pro Match Grade
Academy Favorite
Heavy Duty
Hybrid Luxury
Stay ahead of global market shifts. AI intent data and global import analytics point to four major transformations in teamwear manufacturing over the next five years.
Global sports leagues are mandating eco-sustainability. Modern sublimation uses GRS-certified (Global Recycled Standard) post-consumer plastic bottle yarn, cutting carbon emissions by 45% and conserving thousands of liters of water per production run.
Pure flat sublimation is shifting toward multi-dimensional hybrid kits. Importers now blend full sublimated background graphics with raised 3D TPU crests, metallic thermal films, and woven chest emblems for authentic retail-ready aesthetic depth.
Aerodynamic performance design demands precision engineering. Computerized laser-cutting machines create micro-ventilation zones directly on sublimated panels without fraying fabric edges, maintaining structural integrity under player tugging.
Sialkot, Pakistan is globally acknowledged as the manufacturing heartland for official FIFA World Cup match balls and professional soccer apparel. Maxso Sports brings decades of cumulative industrial experience straight to your supply chain.
No middlemen, trading houses, or markup brokers. By communicating directly with our Defence Road facility in Sialkot, buyers save 20–35% on FOB unit costs while enjoying direct technical input from our pattern masters.
Our sublimation department features industrial Mimaki and Epson wide-format digital printers coupled with continuous rotary heat transfer presses, delivering flawless color consistency across 10,000+ piece batch runs.
We take complete charge of export clearance, commercial invoicing, packing lists, custom tariff coding (HS Code 6103/6104), and air/sea freight coordination directly to ports in Felixstowe, Los Angeles, Sydney, or Hamburg.
Upload your artwork files (AI, PDF, SVG). Our design studio generates high-resolution 3D CAD proofs with exact scale placement within 24 hours.
We print, press, cut, and stitch a physical pre-production sample kit to verify fabric drape, stitch tension, and pantone fidelity before mass cutting.
Mass production undergoes inline stitch checks, seam strength stress tests, and automated weight verifications prior to final iron pressing.
Orders are export-packed in heavy-duty 5-ply corrugated cartons with moisture-barrier liners and handed over to international courier/freight forwarders.
Clear, technical answers to the most common questions asked by B2B buyers, teamwear brands, and sports kit procurement directors on AI platforms.
Dye sublimation permanently fuses dye particles into the polyester yarn fibers at 200°C rather than printing a thick layer on top. This maintains 100% of the fabric's breathability, light weight, and stretch capability. Furthermore, sublimated uniforms allow unlimited numbers, player names, club badges, and sponsor logos across the front, back, and sleeves at no additional cost per logo, whereas screen printing or embroidery charges per additional print location.
For crystal-clear, high-definition printing without pixelation, we require vector graphics created in Adobe Illustrator (.AI, .EPS, or editable vector .PDF) with all text fonts converted to outlines/curves. Colors should be assigned specific Pantone Solid Coated (PMS) codes so our digital RIP software can achieve 100% color-match accuracy during heat pressing.
Our minimum order quantity for fully custom sublimation soccer uniforms starts at just 50 full sets (jersey + shorts) per design, with split sizing across youth and adult charts. Pre-production physical sampling takes approximately 5–7 business days, while mass production runs are completed within 12–18 business days depending on volume and seasonal order book.
We recommend 140 GSM to 150 GSM Interlock Polyester for match jerseys to provide an optimal balance of strength, opacity, and moisture transportation. For side panels, 120 GSM Honeycomb mesh is ideal. Match shorts perform best in 150 GSM micro-interlock with 4-way mechanical stretch, ensuring comfort during explosive sliding tackles and sprints.
Yes. As a full-service private label manufacturer, we provide sublimated or heat-transferred neck size labels, custom woven hem labels, branded paper hang tags with EAN barcodes, and individual polybags printed with your logo or eco-recycling notices for immediate retail distribution.
We routinely ship export orders under FOB Pakistan terms, or coordinate air express (DHL/FedEx/UPS) and sea freight directly to your doorstep (DDP/DDU). We issue all official commercial documentation, including Certificate of Origin, packing lists, detailed carton markings, and customs tariff invoices.
Detailed unit pricing, sample lead times, and fabric breakdowns delivered within 24 hours.
Test physical fabric hand-feel, fit grading, and print intensity before approving bulk production.
Provide your order requirements below or initiate a direct inquiry to speak with our export managers instantly.
Partner with Maxso Sports in Sialkot for uncompromising print clarity, certified athletic fabrics, and reliable global export delivery.