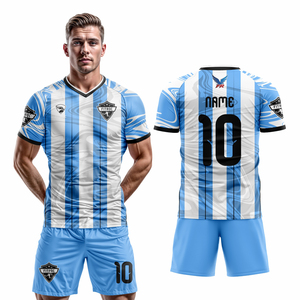
Explore our benchmark custom manufacturing lines. Each item operates as a baseline specification that can be modified according to your club's technical packs, Pantone textile standards, customized cuts, and brand embellishment specifications.
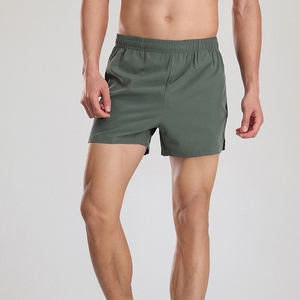
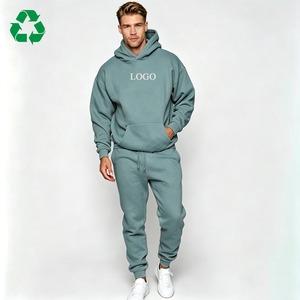
Eliminating middlemen markups and production latency through precision-calibrated digital sublimation, automated cut-and-sew workshops, and integrated trim manufacturing under one roof.
Our sublimation workshops utilize high-precision industrial Japanese print engines (Mimaki and Epson PrecisionCore) coupled with continuous rotary drum calenders. Operating at 210°C under 6.5 bar pressure guarantees gaseous molecular diffusion deep into polyester filaments without surface polymer crusting or breathability loss.
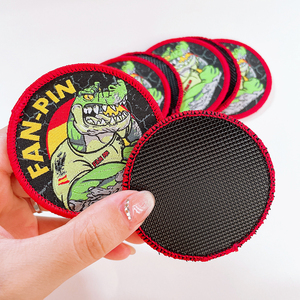
Unlike conventional assemble-only operations, we manufacture woven jacquard club insignias, 3D soft-touch TPU emblems, metallic heat transfers, and custom branded neck tapes internally. This verticality guarantees 100% color synchronization across jersey panels, chest shields, and sleeve bands.
Direct trade processing with comprehensive export clearance capabilities. From pre-shipment third-party lab inspection (SGS/ITS/Bureau Veritas) to automated carton barcoding, custom HS classification coding (6109.90 / 6103.43), and direct bonded warehouse handoffs.
Sublimation quality depends directly on micro-filament engineering. Standard flat polyester often causes sweat saturation and clinging during match play. We engineer custom micro-denier structures engineered for superior capillary evacuation and tensile durability under professional stress.
| Substrate Composition | Knit Construction | Weight (GSM) | Capillary Evaporation | Tensile Burst (PSI) | Color Gamut Fidelity | Ideal Application Tier |
|---|---|---|---|---|---|---|
| 100% Recycled Micro-Poly (rPET) | Interlock Double-Knit | 145 - 155 | 95+ | Ultra-High (108% sRGB) | Pro Match First-Team | |
| 88% Polyester / 12% Spandex | 4-Way High-Stretch Jacquard | 160 - 170 | 110+ | High (98% sRGB) | Compression Match Kit | |
| 100% Virgin High-Filament Poly | Micro Birds-Eye Eyelet Mesh | 135 - 145 | 88+ | High (95% sRGB) | Warm-Weather Tournament | |
| 100% Poly Aerocool Channel | Engineered Waffle Honeycomb | 150 - 160 | 92+ | High (94% sRGB) | Club Academy Wholesale | |
| 92% Micro-Poly / 8% Carbon Yarn | Anti-Static Honeycomb Mesh | 155 - 165 | 105+ | Very High (102% sRGB) | Elite Pro Competition |
The global sports uniform landscape is moving rapidly away from slow, high-inventory mass manufacturing toward closed-loop sustainable polymers, near-instant localized replenishment, and hybrid embellishments.
European and North American legislative frameworks (such as EU Corporate Sustainability Due Diligence) are mandating traceable secondary raw materials. Procurement departments are demanding Global Recycled Standard (GRS) transaction certificates (TC) for post-consumer recycled poly (rPET) derived from oceanic and municipal plastic waste, lowering carbon footprints by 42% per jersey.
The era of holding warehouse deadstock for entire athletic seasons is ending. Clubs and teamwear distributors are adopting agile rolling orders with 50 to 200 unit micro-batches. Combining nested AI layout software with ultra-wide high-speed calendar printers allows factories to turn around personalized roster re-orders in under 72 hours.
Sublimation is no longer isolated to flat print. Leading professional brands combine full-sublimation gradient bases with ultrasonically welded matte TPU club crests, silicone anti-chafing side tape, and laser-perforated dynamic heat-relief zones across the lumbar and thoracic profiles to optimize athlete thermoregulation.
Sporting apparel is integrating flexible micro-NFC chips and woven 2D matrix threads encapsulated into neck labels and hem tags. This provides spectators with interactive fan experiences while providing commercial customs authorities with tamper-proof textile composition and provenance data.
With global bans on per- and polyfluoroalkyl substances (PFAS) taking effect, next-generation outerwear and training jerseys incorporate bio-based C0 hydrophobic finishes that shed rain without impairing the water-vapor permeability index or altering sublimation ink dispersion.
Using computerized jacquard knitting machines, yarn densities transition seamlessly from dense interlock across the shoulders and chest to open-hole ventilation zones along the underarms and spine without requiring physical cut-and-sew panel seams that induce dermal friction.
From raw filament extrusion to final container stuffing, every production run is managed through rigorous standardized quality control checkpoints to guarantee global brand reputation.
Tech packs are parsed into CAD pattern software. Pantone textile codes (TCX/TPX) are converted through RIP ICC profiles. Strike-off swatches are pressed on actual bulk-run polyester yardage and submitted digitally or via express courier for client calibration.
Random sample cuts undergo ISO 105-C06 wash fastness tests (40 cycles at 60°C), AATCC 15 perspiration exposure, and Martindale abrasion cycle evaluations (20,000 revs) to verify no fiber pilling, ink bleed, or cracking across customized crests.
Certified seamstresses execute 4-thread overlock and flatlock reinforcement along high-stress points. Stitching density is checked continuously to maintain 10-12 stitches per inch (SPI), preventing seam popping during competitive tackling and tension pull.
Critical answers regarding minimum order quantities, lead times, sublimation technology, international shipping, and OEM/ODM private-label capabilities.
True industrial dye-sublimation uses heat-activated disperse dye that undergoes endothermic transition directly from solid to gas at approximately 200°C–210°C, chemically bonding inside the synthetic polyester polymer chains. Low-cost direct-to-film (DTF) or vinyl transfers sit on top of the fabric surface as a rubberized polyurethane film. This layer obstructs air permeability, creates heavy chest sweating, and will inevitably crack or peel after multiple high-temperature wash cycles.
For fully sublimated custom team uniforms (jerseys and shorts), our production runs start at 50 units per design split across sizes. For bespoke trims, woven badges, and 3D TPU crests ordered independently, standard batches begin at 100 units. For large-scale multi-club corporate programs or regional sporting tournaments, volume pricing tiers unlock substantial unit-cost efficiencies at 500, 1,000, and 5,000 units.
We do not rely on uncalibrated on-screen RGB visual comparisons. Clients specify Pantone Solid Coated or Pantone Textile (TCX/TPX) color targets. We utilize X-Rite spectrophotometers to calibrate printer ICC color profiles against specific fabric lots under D65 daylight standard light booths. All color formulas and profile parameters are logged in our digital ERP to ensure identical color continuity for future season replenishment batches.
Digital CAD pattern grading and pre-production physical strike-off sampling typically require 7 working days. Once the golden sample is approved in writing, bulk cutting, printing, calender pressing, stitching, quality checking, and individual polybag packaging take 15 to 22 working days for orders between 200 and 2,000 units. Express air freight (DHL, FedEx, UPS) requires 4-6 days, while ocean container shipping spans 18-30 days depending on the destination port.
Yes. We provide complete end-to-end OEM branding: custom branded elastic jacquard waistbands, ultrasonic heat-seal neck labels, FSC-certified recycled cardstock hang tags with custom eyelets and wax cords, branded inner polybags, and master cartons labeled with your club's GS1-compliant logistics barcodes.
Vector files are strictly required to ensure sharp vector edges at full scale. We accept Adobe Illustrator (.AI), Scalable Vector Graphics (.SVG), or print-ready editable PDF formats with all typography outlined. Raster images (JPEG/PNG) must maintain a minimum resolution of 300 DPI at 1:1 scale for photographic background textures to prevent pixelation on full garment panels.
Standard commercial transactions operate on a 30% deposit upon formal Proforma Invoice (PI) confirmation and physical sample sign-off, with the 70% balance payable against final pre-shipment Quality Inspection Reports and Bill of Lading (B/L) copy. Irrevocable Letters of Credit (L/C at sight) are supported for institutional tenders and high-volume container purchase orders.
All base textiles, Italian sublimation inks, and auxiliary threads are strictly certified under OEKO-TEX Standard 100 Class I/II, confirming zero detectable levels of formaldehyde, heavy metals, arylamines, azo dyes, or phthalates. We also supply complete documentation for REACH compliance in the European Union and CPSIA / CA Prop 65 standards in North America.
Eliminate production delays, inconsistent color reproduction, and poor fabric performance. Partner with an established Chinese manufacturing leader equipped to manage your tech packs from digital strike-off to international port delivery.