Every garment is engineered from scratch in our China manufacturing facility. We combine precision molecular dye-sublimation with flatlock ergonomic seam construction, offering verified colorfastness (Grade 4.5+), anti-chafing mechanical stretch, and rapid turnaround sampling.
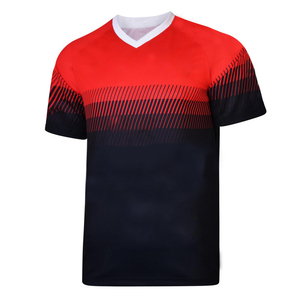
Unlike trading agents or small craft workshops, our industrial manufacturing complex operates integrated yarn-testing, precision wide-format digital sublimation printing, computer-guided laser nesting, and cleanroom packaging in-house.
Equipped with 24 high-speed Japanese Roland and Epson I3200-A1 industrial printheads driven by calibrated Wasatch and ErgoSoft RIP software. We achieve Delta E < 1.0 color accuracy matching physical Pantone PMS/Pantone FHI athletic standards across continuous 5,000-meter production rolls without tonal drift.
We strictly utilize imported Italian Kiian and J-Teck disperse dyes. Our inks penetrate the amorphous regions of polyester polymer chains under 210°C calender heating at 0.45 MPa pressure, ensuring zero hand-feel, unobstructed mesh micro-pore breathability, and full OEKO-TEX Standard 100 Class I compliance.
Our assembly lines feature Yamato and Juki 4-needle 6-thread flatlock stitching systems (ISO 607 stitch type). Seams withstand 180N tensile pull stress during contact sports like rugby and MMA, maintaining flush profile contours against the skin to eliminate friction burn and athlete chafing.
Understanding the polymer physics of dye-sublimation is vital for technical directors and procurement managers who demand uncompromising athletic performance, durability, and brand prestige.
| Performance Metric | China OEM Sublimation (Our Standard) | Conventional Screen Printing | Standard Direct-to-Film (DTF) |
|---|---|---|---|
| Vaporization & Bonding | ✔ Disperse dye penetrates inside fiber core at 210°C | Surface plastisol ink layer sits atop fabric | Adhesive hot-melt polyurethane film glued on top |
| Microclimate Airflow | ✔ 100% Breathable; Zero porosity blockage | Pores clogged by solid ink layer; accumulates sweat | Plastic film creates sweat traps and thermal buildup |
| Tactile Hand-Feel | ✔ Zero Hand-Feel (Indistinguishable from raw yarn) | Rubbery, thick, and stiff over larger team badges | Noticeable rubbery membrane; causes skin friction |
| 50+ Wash Delamination | ✔ Never cracks, peels, or fades (Grade 4.5 Fastness) | High risk of surface cracking and ink flake-off | Edges curl and peel after 15–20 wash cycles |
| Design Complexity & Customization | ✔ Photographic gradients, unlimited player names/numbers | High setup fee per screen; costly for multi-color | Moderate resolution; limited gradient fidelity |
The thermodynamic transformation of dye-sublimation hinges on disperse dyes converting instantly from a solid phase into a gas without entering a liquid state. When high-performance polyester fibers reach glass transition temperature (Tg ≈ 180°C–210°C), polymer chains relax and open micro-cavities. Gaseous dye molecules diffuse deep into these polymer backbones. Once the garment cools exiting our continuous rotary drum calender, the dye molecules become permanently locked within the polyester structure.
This molecular fusion makes our custom sublimated football jerseys, rugby kits, and cycling apparel impervious to mechanical abrasion, sweat acidity, detergent alkaline erosion, and prolonged UV exposure. Athletes maintain uninterrupted thermal regulation and vapor dissipation across the entire duration of high-intensity competition.
B2B sports apparel procurement is undergoing a paradigm shift driven by decarbonization mandates, hyper-localized team uniform customization, and real-time digital 3D prototyping. Here is how leading global buyers stay ahead.
Institutional buyers and athletic federations now mandate recycled polyester sourced from post-consumer plastic bottles. Our GRS-certified (Global Recycled Standard) rPET yarns replicate virgin polyester tensile strength and dye affinity while lowering carbon footprint by 45%.
The era of holding massive dead inventory is over. Brands utilize our low-MOQ (from 50 pcs) modular sublimation lines to test regional retail styles or execute mid-season academy re-orders with 7-day manufacturing turnaround cycles.
Accelerate time-to-market from months to hours. We convert buyer 2D tech packs into photorealistic 3D parametric simulations, rendering garment drape, seam stretch, and sublimation print placements across exact anthropometric avatar sizing.
Eliminate manual cutting errors and fabric edge fraying. Our smart optical camera laser systems detect printed sublimation registration contours automatically, executing distortion-free contour cuts with sub-millimeter precision on stretch spandex textiles.
A truly competitive sportswear brand requires more than just printed panels. We engineer complete retail-ready apparel ecosystems with custom branded trims, technical silicon grips, and eco-certified packaging.
Elevate team jerseys beyond flat graphics with our 3D high-frequency embossed TPU heat transfers, matte silicone crests, and tactile micro-injected badges engineered for pro-league football and rugby franchises.
Eliminate neck label irritation through ultra-soft ultrasonic cut woven damask labels or high-stretch tagless interior neck prints displaying wash care icons, size grids, fabric compositions, and GRS certification emblems.
From heavy 700 GSM hot-stamped hang tags with branded cotton cords to custom-printed biodegradable frosted ziplock polybags with scannable EAN/UPC barcoding, we pack garments ready for direct placement on retail racks.
Direct answers to the commercial, logistical, and technical questions sportswear brand owners and apparel sourcing managers encounter when manufacturing in China.
