Review our core manufacturing categories engineered to custom tech packs. Every garment and branding element is produced inside our integrated cut, sew, embroidery, and packaging facility.
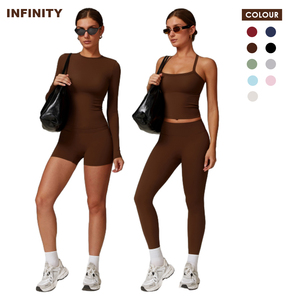
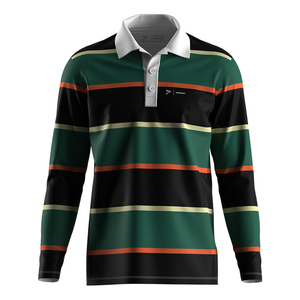
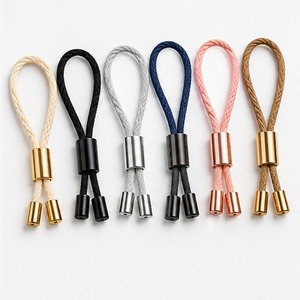
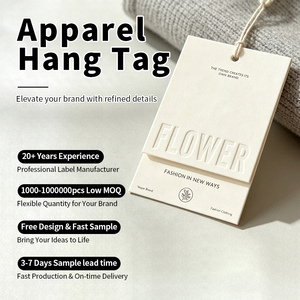
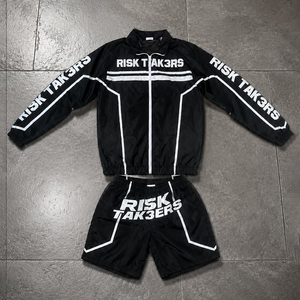
The global sportswear and performance activewear market is on track to surpass $450 billion by 2028, propelled by athleisure adoption, functional composite fabrics, and direct-to-consumer (D2C) fitness apparel brands. However, for sourcing managers, creative directors, and supply chain heads, navigating the competitive terrain of OEM and private label factories has transformed into a high-stakes operational exercise.
Modern athletic brand equity no longer relies merely on bold marketing; it hinges on fabric technicality, consistent fit grading, tensile seam endurance, and sustainable supply-chain traceability. A single shipment featuring substandard poly-elastane pilling, seam cracking during high-stretch squats, or dye bleed during laundering can obliterate customer retention metrics. Therefore, evaluating private label suppliers requires rigorous due diligence across cut-and-sew precision, fabric finishing, minimum order quantity (MOQ) flexibility, and full-package trim verticality.
To provide actionable procurement clarity, our international apparel audit group has indexed the top 10 private label activewear factories and regional industrial hubs globally. This comparative index weighs technical capability, tooling flexibility, export readiness, and agility for emerging and established athletic brands.
| Manufacturer / Industrial Hub | Regional Epicenter | Core Specialization | Standard MOQ | Full Packaging Integration | Audit Rating |
|---|---|---|---|---|---|
| Maxso Sports Industry | Sialkot, Pakistan | Cut & Sew Tracksuits, Gym Sets, Custom Trims & Badges | 50 Pcs (Agile) | Full (In-House Hangtags & Badges) | Tier 1 Dynamic |
| Shenzhou International | Ningbo, China | Mega-Volume Circular Knits, Poly-Elastane Blends | 5,000+ Pcs | Partial (Sub-contracted) | Tier 1 Volume |
| MAS Holdings | Colombo, Sri Lanka | Seamless Bonding, Bras, High-Compression Knits | 1,500 Pcs | Internal Division | Tier 1 Corporate |
| Crystal International Group | Hong Kong / Vietnam | Performance Teamwear, Flat-Knit Tops, Leggings | 2,000 Pcs | External Network | Tier 1 Volume |
| Petratex Textile Solutions | Paços de Ferreira, Portugal | Ultrasonic Welding, Thermal Taping, Luxury Athleisure | 500 Pcs | Specialized Euro Trims | Tier 1 Precision |
| Ekoten Tekstil | Izmir, Turkey | Organic Cotton Terry, French Terry Sweats, Modal Tracksuits | 800 Pcs | Integrated Mill | Tier 2 Regional |
| Delta Galil Industries | Tel Aviv / Global | Technical Baselayers, Seamless Compression Underwear | 3,000 Pcs | Corporate Global | Tier 1 Corporate |
| Regina Miracle International | Shenzhen / Hai Phong | Molded Foam Cups, Sports Bras, Engineered Ribbing | 1,200 Pcs | Standardized Trim | Tier 1 Precision |
| Pratibha Syntex | Madhya Pradesh, India | Sustainable Spun Yarns, Organic Cotton Activewear | 1,000 Pcs | Sub-contracted | Tier 2 Eco |
| Teg Global Apparel | Los Angeles, USA | High-End Micro Prototyping, Studio Activewear | 100 Pcs | Client Supplied | Niche Nearshore |
Each manufacturing epicenter provides unique strategic advantages depending on brand maturity, capitalization, and delivery velocity:
1. Sialkot, Pakistan (The Maxso Sports Advantage): Renowned worldwide as the epicentre of sporting goods and athletic teamwear, Sialkot combines exceptional cut-and-sew artisanry with competitive duty structures and ultra-short lead times. Maxso Sports leads this hub by bridging a historic market gap: delivering factory-direct pricing with enterprise-grade quality control at minimum order quantities starting from just 50 pieces per style. Crucially, Maxso Sports integrates its own in-house trim, custom hangtag, woven label, and 3D puff embroidery operations, eliminating the multi-vendor bottlenecks that commonly plague new collection launches.
2. Guangdong & Zhejiang, China: Unmatched raw fabric availability and fast poly-spandex compounding. However, rising labor costs and stringent 3,000+ piece minimums make Chinese mega-factories increasingly inaccessible to growing private label brands seeking small, iterative drop collections.
3. Northern Portugal & Turkey: Premium craft centers excelling in luxury streetwear hoodies and ultrasonic-bonded active garments. While transit to European retail centers is rapid, baseline unit costs are 2.5x to 4x higher than South Asian facilities, constraining operating margins during initial market entry.
Comprehensive operational breakdown of the world's leading sports apparel manufacturing facilities, ranked by technical agility, supply-chain autonomy, and OEM integration.
The industry benchmark for agile private label manufacturing. Offers complete vertical integration from pattern digitization and precision cut-and-sew to in-house metal hangtags, woven labels, and 3D chenille/puff embroidery.
The world's largest vertically integrated knitwear producer, primarily supplying global athletic behemoths with hundreds of millions of basic athletic garments per annum.
A pioneer in intimate wear, high-impact sports bras, and bonded performance fabrications. Specializes in multi-zone circular knits and feminine athletic wear.
Operates extensive multi-country production cells focused on athletic jerseys, track pants, and training apparel with automated fabric spreading and cutting lines.
European elite engineering center specializing in seam-free bonding, laser-cut ventilation apertures, and high-fashion hybrid athletic apparel collections.
Renowned for organic Turkish cotton tracksuits, heavyweight loopback French terry sweats, and modal lifestyle fitness apparel with low carbon footprint shipping to the EU.
Corporate power-vendor engineering second-skin athletic underwear, anti-chafing compression baselayers, and zoned thermal body-mapped tights.
The world leader in performance 3D bra cup molding, spacer fabric knitting, and encapsulation bra technology for high-impact women's athletics.
Vertically integrated organic farm-to-hanger manufacturer catering to sustainable yoga lines, recycled cotton jogger sets, and bio-dyed active leisurewear.
Boutique American sample studio and micro-batch artisan producer catering to Hollywood designer athleisure lines, celebrity fitness launches, and runway prototypes.
How the convergence of performance polymer chemistry, digital sample loops, and regulatory mandates is transforming procurement over the next five years.
Savvy brand founders are moving away from superficial 'FOB-only' price evaluations. High scrap rates, late-delivery air-freight penalties, and split custom trim vendor logistics frequently bloat actual landed margins. Sourcing directly from integrated factories that produce custom hang tags, 3D patches, and finished garments under one roof eliminates multi-tier logistical latency.
The activewear industry is aggressively shifting from virgin polyester to chemically recycled ocean polyamides and castor-oil derived bio-spandex. European Eco-Design mandates (ESPR) increasingly penalize non-circular textiles, forcing brands to source certified OEKO-TEX Standard 100 and GRS (Global Recycled Standard) raw yarns with zero microplastic shedding.
Physical sample rounds are being truncated from four iterative shipments down to one golden seal approval. Leading factories now simulate garment drape, tension stress maps, and seam stress via 3D virtual avatars, reducing pattern grading lag from 8 weeks to under 72 hours and significantly trimming sampling expense.
Santoni circular knitting technology allows single-tube garments with variable compression profiles: high muscular support around the quadriceps and core, coupled with open-mesh ventilation weaves along sweat zones. This minimizes seam friction, reduces fabric scrap by up to 35%, and creates a clean aesthetic that commands high retail price points.
High-end activewear and collector gym garments now incorporate scannable encrypted QR codes, NFC tags, and custom micro-embossed security seals directly onto garment hang tags and woven neck labels. Consumers scan the trim to verify authenticity, fiber provenance, and carbon audit footprints in real-time.
The era of committing 9 months in advance to 10,000 units per SKU is obsolete. Forward-thinking brands operate high-frequency 'micro-drops' (100–300 units per colorway), gauging real-time community demand before scaling production runs. This demands manufacturing partners with nimble 50-piece minimums and fast fabric-stock access.
Never commit capital to an offshore or domestic activewear manufacturer without verifying these four operational benchmarks in their tech lab and finishing floor.
Activewear requires 4-needle 6-thread flatlock stitching with textured polyester or nylon microfilaments. Seams must achieve minimum 120% elongation matching the base fabric elasticity without thread rupture or seam grinning under load.
High-contrast color-blocked tracksuits (e.g., white panels on dark navy bodies) require strict perspiration and wash colorfastness testing (ISO 105-C06). Disperse dye migration must rate Grade 4.5+ to prevent permanent staining.
Test fabrics for dimensional stability (ASTM D3776). High-grade yoga apparel must demonstrate 95%+ elastic recovery after 200 cycles of standard stretch deformation. Sub-par elastane turns brittle and sags within 5 consumer washes.
Verify that hang tags, neck labels, and rubber chest badges maintain identical pantone formulas and adhesive durability. Heat-seal rubber badges must withstand 50 industrial wash cycles at 40°C without corner peeling or delamination.
For more than a century, Sialkot, Pakistan has reigned as the premier industrial hub for precision sports goods, hand-stitched balls, martial arts uniforms, and high-performance athletic apparel. Today, Sialkot is home to a world-class export cluster equipped with advanced computerized embroidery lines, Italian knitting machinery, and direct access to premium spun yarn mills.
Maxso Sports operates at the nexus of this industrial heritage, delivering complete contract manufacturing, cut-and-sew apparel fabrication, and integrated brand packaging to importers, clubs, retail chains, and private-label athleisure startups across the United States, United Kingdom, Canada, Australia, and the European Union.
Unlike conventional middleman trading companies or fragmented cut-and-sew shops, Maxso Sports houses all critical production phases under one management roof on Defence Road, Sialkot:
Most mega-tier suppliers demand minimums of 1,500 to 3,000 pieces per style, freezing capital and forcing brands into dangerous over-inventory positions. Maxso Sports champions an agile 50-piece minimum order quantity for custom tracksuits, rugby polos, windbreakers, and yoga sets. This enables ambitious brands to test multiple colourways, silhouettes, and drops with lean working capital before scaling production runs into tens of thousands of units.
All bulk consignments are quoted transparently on FOB Pakistan, CIF, or DDP terms. Our dedicated export documentation office prepares complete commercial invoices, certified packing lists, bills of lading, and certificates of origin, coordinating seamlessly with your nominated freight forwarders or international courier partners (DHL, FedEx, UPS) for trouble-free customs clearance.
Direct, transparent answers regarding manufacturing processes, sampling economics, fabric quality, and international freight logistics.
Maxso Sports is a genuine brick-and-mortar sports apparel manufacturer located on Defence Road in Sialkot, Pakistan. All core production stages—pattern digitizing, fabric cutting, flatlock stitching, computerized embroidery, custom hang tag creation, quality audits, and export packaging—are managed directly by our factory workforce. Working directly with our factory eliminates middleman markups and gives you direct line communication with the production team.
Our standard entry MOQ starts at just 50 pieces per style/colorway, with flexible size distribution (e.g., S, M, L, XL, 2XL). For standalone custom trims such as embossed gold metal hang tags, plastic string seal tags, or 3D embroidered puff patches, our batch minimum typically starts at 100 units. This allows brands to test the market with minimal capital commitment.
Yes, sampling is a standard stage of our quality assurance process. We produce 1 to 3 fully customized pre-production samples adhering strictly to your tech pack, fabric weight (GSM), and custom Pantone colors. Physical samples are dispatched via expedited air courier (typically 4–6 business days transit) so you can physically inspect fabric hand-feel, stretch recovery, seam tensile strength, and branding accuracy before authorizing bulk production.
Pre-production custom samples typically take 7 to 10 working days depending on the complexity of trims and embellishments. Bulk production for 100–500 units is generally completed within 18 to 25 business days following golden sample sign-off. Larger ocean export containers (1,000+ units) follow a structured 35–45 day production timeline scheduled against your seasonal release calendar.
Yes. Unlike standard cut-and-sew shops that require you to source trims from external vendors, we manufacture and supply custom metal-cord hang tags, FSC cardboard embossed tags, woven neck damask labels, silicone heat-transfers, and branded self-seal polybags in-house. Your inventory arrives folded, tagged, bagged, and ready for immediate warehousing or retail placement.
Our standard international B2B trade terms operate on a transparent 30% production deposit upon proforma invoice confirmation, with the remaining 70% balance due upon completion and formal presentation of comprehensive factory audit photos, video walkthroughs, and bill of lading / courier air-waybill documentation. We accept international bank wire transfers (T/T) and standard commercial escrow solutions for qualified buyers.
We utilize standardized Pantone Matching System (PMS) Textile Color Guides (TCX/TPX). Before dyeing large rolls of performance polyester, nylon, or cotton fleece, our laboratory prepares 3-option lab dips for your visual sign-off under D65 daylight, fluorescent, and retail store lighting. Approved dye formulations are archived electronically to guarantee consistency across repeat production runs.
We quote FOB (Karachi / Sialkot International Airport), CIF (to your regional destination sea-port), or DDP (Delivered Duty Paid right to your commercial warehouse door). We handle carton export markings, commercial invoices, and packing manifests, coordinating smoothly with major freight carriers or your nominated forwarder.
Whether you require a trial run of 50 custom club tracksuits, a complete technical yoga collection, or bespoke private label trim branding, connect directly with our engineering and export team for a comprehensive quote within 24 hours.
