Examine our active production lines, athletic trim engineering, and specialized sportswear packages. Every product reference is precision-manufactured with premium yarn compositions, high-density stitching, and customizable branding solutions tailored for low-MOQ rapid launches and bulk distribution alike.
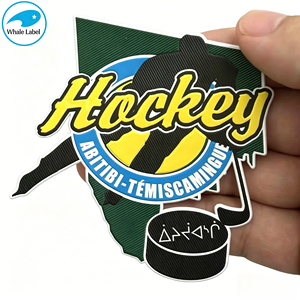
Engineered for technical gym garments and pro match kits. Delivers dimensional relief with anti-abrasion durability under rigorous athletic conditioning.
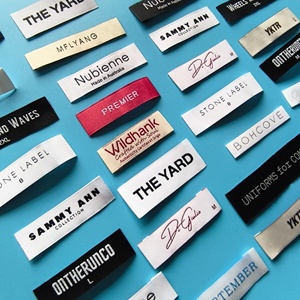
High-density thread count eliminates skin irritation during high-intensity training. Critical for establishing institutional luxury across activewear lines.
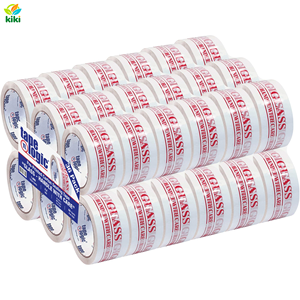
Reinforces custom e-commerce unboxing experiences for fitness DTC startups and enterprise wholesale export logistics consolidation.
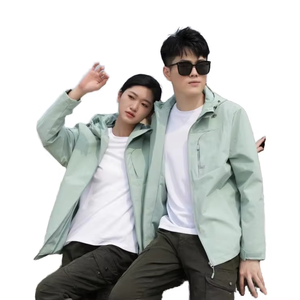
Thermal control windbreaker specifically constructed for outdoor athletic warmup runs and track training, featuring secure utility compartments.
Maintains structural retention without cracking under four-way stretch athletic fabric movements in pro team jerseys and gym compression tops.
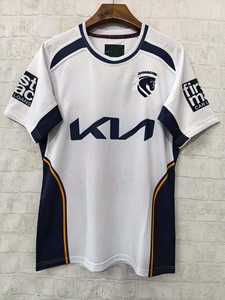
Engineered for high-impact functional fitness, powerlifting, and rugby matches. Features moisture-dispersing yarns with zero color degradation.
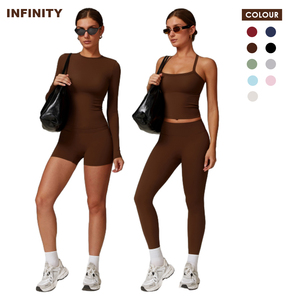
Core private label bestseller. Features a zero-slip high waistband, continuous muscle contouring, and moisture-wicking capillary fiber matrix.
The industry benchmark for premium gym hoodies, athletic caps, and performance jackets. Eliminates needle penetrations while maintaining elasticity.
Operating directly out of the globally acknowledged sporting goods industrial epicenter in Sialkot, Pakistan, our manufacturing facilities integrate tech-pack pattern drafting, precision laser cut-and-sew, proprietary decoration suites, and end-to-end export documentation under one single chain of custody.
Unlike digital middlemen or trading agencies that introduce massive markups and disjointed communications, you negotiate directly with our factory floor managers on Defence Road. This yields unmatched cost transparency, instantaneous tech-pack revisions, and uncompromised QC authority over yarn selection and dye lot consistency.
Gym wear demands specialized mechanical integrity. We deploy state-of-the-art Japanese 4-needle 6-thread flatlock stitching systems, digital pattern CAD grading across bespoke Western sizing charts (EU, UK, US), and specialized interlock seam reinforcement to guarantee anti-burst resilience across heavy squat, stretch, and sprint loads.
We eliminate the legacy barrier of 1,000-piece production minimums. Our modular cell workflow allows private label fitness startups and fast-moving gym brands to launch new colorways and styles with realistic minimums starting from 50 pieces per design, allowing lean testing before scaling up to high-volume commercial production.
From Italian sublimation ink systems that penetrate deep into polyester synthetic fibers without fading, to 3D heat-pressed TPU badges, ultra-plush varsity chenille embroidery, and silicone micro-injections—all embellishments are crafted within our localized supply chain to ensure precise Pantone color matching and zero delamination.
Every commercial order is anchored by comprehensive pre-production sampling. We formulate physical sample garments within 7–10 working days, providing complete fit tests, stitch elongation checks, and hand-feel validations. Once signed off, the physical sample serves as the binding quality metric for our inline QA inspectors.
Our dedicated export department handles complete documentation in-house: Commercial Invoices, GSP Forms, Packing Lists, and Bill of Lading certifications. We orchestrate containerized ocean freight and rapid courier air shipments directly into key ports throughout the United Kingdom, United States, Canada, Australia, and the European Union.
The international athletic apparel landscape is transitioning from rudimentary contract manufacturing toward hyper-agile, transparent, and technology-driven supply chains. Brand directors and procurement executives must align with these shifting institutional dynamics to protect margins and secure consumer relevance.
While Western brands experiment with nearshoring to decrease transit timelines, production costs and specialized stitch craftsmanship remain uncompetitive in domestic regions. The prevailing global sourcing strategy couples agile, high-dexterity export hubs like Sialkot with pre-booked fabric allocations. This enables rapid 25-day production sprints while preserving gross manufacturing margins between 60% and 75%.
The post-inventory crisis era has rendered multi-thousand unit speculative volume dead on arrival. Modern activewear directors now procure in staggered seasonal releases—initiating capsule collections in 100-to-300 piece drops. Factories providing responsive sub-assembly cell configurations give brands the ability to replenish out-of-stock sizes within three weeks, radically optimizing working capital velocity.
Physical sampling iterations generate unnecessary carbon footprints and burn months of lead time. Leading athletic factories now accept and manipulate CLO3D, Browzwear, and Optitex virtual rendering files directly. Virtual tension maps visualize seam pull and compression pressure across 3D avatars, allowing technical revisions to be confirmed digitally prior to the very first physical fabric cut.
With the European Union's Corporate Sustainability Due Diligence Directive and stricter US Uyghur Forced Labor Prevention Act (UFLPA) enforcement, gym wear procurement requires auditable chain-of-custody documentation. Sourcing agents must authenticate yarn origins, GRS (Global Recycled Standard) certifications for recycled polyester, and OEKO-TEX Standard 100 chemical safety records for all synthetic dyeing agents.
Sourcing garments from one vendor and rubber patches, woven neck labels, and packaging tape from another leads to catastrophic assembly bottlenecks. Strategic buyers are consolidating procurement exclusively with integrated factories that engineer the primary apparel line and trim components under one unified production schedule, ensuring color-matching precision and synchronized delivery.
Next-generation activewear requires a sophisticated synthesis of polymer science, ergonomics, and aesthetic luxury. Today's consumers demand apparel that performs under peak biomechanical strain while transitioning seamlessly into lifestyle athleisure settings.
Modern gym apparel is shifting away from generic ring-spun polyesters to micro-denier synthetic matrices. By combining 75D/72F micro-polyester or high-filament nylon 6.6 with cross-section channel fibers, sweat is mechanically pulled via capillary pressure from the inner epidermis to the outer garment layer, achieving Moisture Vapor Transmission Rates (MVTR) exceeding 8,500 g/m²/24hr.
Utilizing high-gauge Santoni seamless knitting machines, we weave multi-density compression structures directly into single continuous fabric tubes. This engineering eliminates side seams entirely, strategically integrating open-mesh ventilation zones along sweat corridors (lumbar and underarm) while concentrating high-elasticity tension rings around core muscular anchor points.
Bacterial odor buildup in synthetic activewear remains the leading cause of customer dissatisfaction. We apply EPA-approved silver-ion chloride finishes and non-toxic zinc pyrithione solutions during bath dyeing. The active antimicrobial agent binds directly within the yarn structure, inhibiting bacterial proliferation and preserving freshness over 50+ commercial wash cycles.
For ultra-lightweight running gear and compression base layers, needle perforations can cause chafing. We utilize high-frequency ultrasonic welding combined with thermo-polyurethane seam-sealing bonding tapes. This produces completely flat, needleless joints that possess twice the tensile burst strength of traditional overlock stitching while dropping garment weight by 15%.
The convergence of activewear and biometric performance monitoring is reshaping technical gym apparel. Our development teams are prototyping laminated conductive fabric tracks and elastic silicone sensor pockets engineered into sports bras and compression tights, capable of housing Bluetooth telemetry pods without restricting muscular elasticity.
Transparent technical standards separating true high-performance sportswear manufacturing from baseline commercial apparel printing. Review our internal engineering tolerances:
| Performance Dimension | Commercial Sialkot Standard | Baseline Trading House Spec | B2B Quality Benefit |
|---|---|---|---|
| Fabric Weight (GSM) Tolerance | ± 3% Electronic Gram Scale | ± 10% Unverified Batch | Eliminates sheer, see-through tights and unexpected heavy winter drape. |
| Colorfastness (AATCC 61-2A) | Grade 4.5+ (50 Wash Cycles) | Grade 3.0 (Fades after 10 washes) | Prevents color bleed across contrast panels during intense hot machine washes. |
| Seam Rupture Elasticity | 120% Seam-to-Fabric Match | 80% (Risk of thread snap) | Guarantees 100% squat-proof elasticity under heavy powerlifting biomechanics. |
| Dimensional Stability (Shrinkage) | < 2.0% Length & Width | 5.0% – 7.5% Uncontrolled | Preserves original garment fit and grading integrity after domestic tumble drying. |
| Embellishment Peel Resistance | 3.5 N/mm (ASTM D903) | 1.2 N/mm Hand-ironed | TPU badges and heat transfers will never crack, curl, or peel off during workouts. |
Practical, direct operational guidance addressing critical supply chain variables, commercial payment terms, factory compliance, and import logistics for wholesale apparel buyers.
Bypass intermediary markups, mitigate inventory liabilities, and take full control over your technical specifications. Connect directly with our Sialkot factory engineering and export logistics team to receive an itemized commercial quotation, fabric swatch options, and sample development schedules within 24 hours.
