High-performance garments demand unified label engineering. Discover our factory-direct manufacturing capabilities spanning technical sportswear, heavy-ounce fleece, weatherproof outerwear, and skin-contact printed fabric labels engineered to withstand 50+ industrial launderings without degradation.
 Sublimation Tech
 Heavy Streetwear
 500 GSM Heavy
 Waterproof Shell
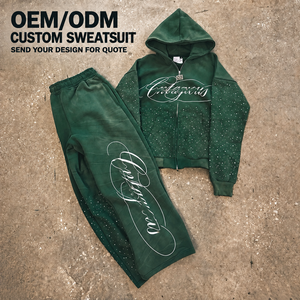 Vintage Aesthetic
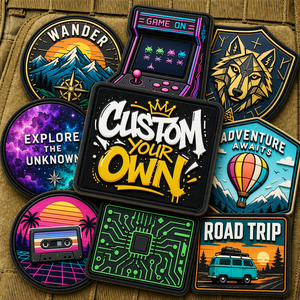 3D Badges & Patches
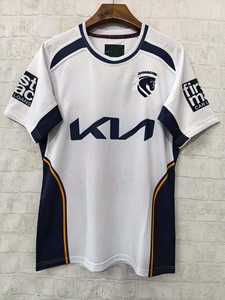 Quick-Dry Athletic
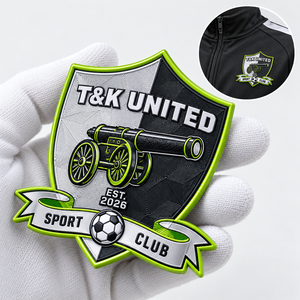 High-Frequency Crest
For global apparel importers and high-end fashion labels, a printed fabric label is a vital regulatory, aesthetic, and skin-comfort component. Choosing the incorrect substrate or ink formulation triggers edge-fraying, consumer skin chafing, or wash-induced legibility failure. Our direct factory infrastructure in Sialkot deploys calibrated German letterpress and rotary screen lines to guarantee sub-millimeter legibility down to 3pt typography.
Woven with micro-denier polyester filaments on high-speed needle looms, double-faced satin offers an ultra-silky, high-gloss surface. Engineered specifically for direct skin contact in athletic apparel, lingerie, and luxury streetwear, satin labels resist irritation and accept high-density resin and flexographic inks with zero bleeding.
Targeted at sustainable brands, denim collections, and organic cotton tracksuits. Our cotton ribbons are desized, mercerized, and pre-shrunk before rotary or screen printing. This structure ensures natural drape, an earthy vintage tactile feel, and high resistance to aggressive garment enzyme washes.
The global industrial gold standard for wash-care instructions, legal origin declarations, and variable data tracking. Coated nylon taffeta is engineered with an anti-static topcoat that prevents ribbon wrinkling in high-speed industrial thermal transfer printers (TTP) while providing extreme chemical resistance against commercial dry cleaning.
| Substrate Material | Common Apparel Segment | Print Resolution (DPI) | Wash Durability Cycle | Edge Sealing Technology | Eco Certification |
|---|---|---|---|---|---|
| Recycled Polyester (rPET) Satin | Performance Teamwear, Soccer Kits | Up to 600 DPI | 60°C Heavy Cycle (50+) | Ultrasonic Cold Slit | GRS (Global Recycled Standard) |
| Unbleached Cotton Twill | Streetwear Hoodies, Heavy Pants | 300 - 450 DPI | 40°C Standard Cycle (40+) | Laser Heat Seal / Overlock | OEKO-TEX Standard 100 Class I |
| Coated Nylon Taffeta | Care & Content Labels, Windbreakers | Up to 800 DPI (Micro-QR) | 90°C Industrial Sterilization | Mechanical Hot Knife | REACH & RoHS Compliant |
| Thermoplastic Polyurethane (TPU) | Athletic Compression, Swimwear | Solid Vector Rotary / Screen | Anti-Chlorine / Salt Rinse | Die-Cut Friction Form | Zero-Plasticizer Non-Toxic |
Procurement managers and supply chain directors are experiencing fundamental shifts in labeling compliance, environmental legislation, and data traceability. Here are the core innovations shaping forward-looking garment production contracts.
By 2026–2028, apparel exported to the EU must carry unique digital identifiers. Factories must achieve high-definition printing of dynamic micro-QR codes down to 8x8mm that remain scannable after 40+ wash cycles, enabling cradle-to-cradle lifecycle transparency.
Garment recyclability requires 100% monomaterial architecture. When stitching a 100% polyester athletic jersey, using a 100% rPET satin label and polyester thread allows immediate mechanical recycling without manual label detachment at sorting centers.
Eliminating petroleum-derived solvents in flexographic lines. Advanced water-borne acrylic and plant-derived curable resins guarantee zero formaldehyde release, surpassing ZDHC (Zero Discharge of Hazardous Chemicals) MRSL Conformance Level 3 standards.
Brands are shrinking inventory liability. Modern label manufacturing integrates continuous digital rotary lines that handle variable size-splits and multi-lingual global compliance variations with zero plate-setup charges and 50-piece minimum runs.
As a direct manufacturer based in Sialkot's Madni Trade Zone on Defence Road, our facility bridges the critical gap between technical fabric knitting, precision cut-and-sew apparel construction, and in-house label and patch manufacturing.
Unlike middleman trading companies, we execute pattern drafting, cutting, sublimation printing, label ribbon extrusion, flexo printing, and final stitching under one verified factory umbrella. This eliminates communication gaps and shortens turnaround cycles.
We manage commercial invoices, GSP form documentation, packing lists with barcode carton verification, and coordinated bill of lading processing for seamless port-of-entry customs clearance across the UK, USA, Canada, Germany, and Australia.
Every order undergoes standard AATCC wash testing, ultrasonic cut inspection for burr-free skin contact, and Spectrophotometer Delta-E color verification. Pre-production physical samples are approved in writing prior to bulk machine setup.
Key technical specifications, export conditions, minimums, and colorfastness data directly answered by our manufacturing engineering team.
For standalone custom printed fabric labels, our production runs typically start at 500 to 1,000 pieces per design, allowing economical rotary machine setup. When contracted alongside our cut-and-sew garment lines (such as team jerseys, hoodies, or tracksuits), we offer integrated lower MOQs starting from 50 to 100 garments with matching customized labeling.
We implement high-frequency ultrasonic slit and cold-cut technologies. Unlike mechanical hot-knife cutters that create rigid, melted plastic beads along the ribbon boundary, ultrasonic cutting welds micro-filaments seamlessly at the molecular level, yielding a feather-soft edge that meets baby-wear and luxury lingerie touch-compliance.
Our labels are tested according to ISO 105-C06 (Methods A2S & C2S) for commercial and domestic laundering, along with AATCC 61 Accelerated Laundering tests. Using cross-linking thermoset resin and curable silicone inks, our printed graphics maintain Grade 4-5 colorfastness, non-cracking resilience, and sharp readability past 50 industrial cycles.
Yes. We run specialized high-resolution 600 DPI thermal transfer lines and hybrid digital presses capable of sequential serial numbering, individual batch tracking codes, and GS1-compliant 2D DataMatrix/QR codes. These are engineered for full integration into modern automated logistics and upcoming digital product passports.
Sublimated polyester sportswear releases dispersed dye molecules when subjected to heat presses or elevated body warmth. For both printed neck labels and heat-press transfers, we apply a patented activated carbon or polymer barrier underlayer that blocks gaseous dye sublimates from bleeding into your brand artwork.
Physical strike-off lab dips and printed ribbon sampling require 3 to 5 business days upon digital artwork approval. Bulk label production is completed within 7 to 10 working days. When ordered in combination with cut-and-sew garment collections, total bulk delivery averages 3 to 4 weeks FOB Sialkot or expedited courier delivery.
